Business Details
34 Years
experience
Custom Culinary Products for Restaurants & Food Brands
Established in 1992, Haliburton has dedicated itself to merging culinary excellence with advanced food science and technology. Our strategically located facility in Ontario, California, operates within North America's agricultural heartland, enabling access to fresh, high-quality ingredients. With a 300,000-square-foot manufacturing space processing over 50 tons of food hourly, we specialize in crafting custom, restaurant-grade products such as fire-roasted vegetables, globally inspired sauces, artisan soups, and innovative beverage mixers. Our commitment to quality is validated through 50 annual independent food safety inspections, ensuring compliance with the highest industry standards.By continuously investing in cutting-edge processing and packaging technologies, we empower multi-unit restaurant operators and retailers to deliver distinctive, scratch-quality menu solutions with operational efficiency. Our team of culinary experts and food scientists collaborates to develop tailored products that meet specific client needs while maintaining rigorous quality assurance protocols, including on-site microbiology and physical chemistry labs. This dedication to innovation, quality, and customer-centric service has solidified our reputation as a trusted partner for some of the world's most recognized food brands.
Services
Fire Roasted Vegetables
Pickled Vegetables
Kettle Cooked Sauces
Artisan Soups
Craft Beverage Mixers
Breakfast Scrambles
Authentic Salsas
Condiments & Dips
Dessert Sauces
IQF Grain Blends
Details
- Year established: 1992
Highlights and features
- We have 30+ years of experience in custom food product development
- Our proprietary flame roasting and flash freezing process preserves freshness
- We maintain on-site microbiology and chemistry labs for quality assurance
- We process over 50 tons of fresh food hourly with USDA/FDA licenses
- Our team includes expert chefs and food scientists working collaboratively
Services
Fire Roasted Vegetables
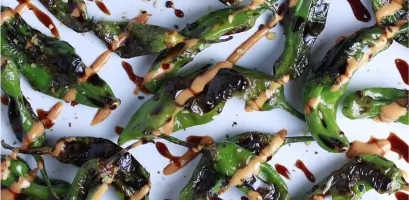
Our proprietary flame roasting and flash freezing process preserves the natural flavor, color, and texture of over 20 vegetable varieties. Using high-temperature roasting techniques, we deliver consistent quality for foodservice operators seeking scratch-made quality with convenience. Our capabilities include sweet bell peppers, mushrooms, asparagus, and exotic fruit options.
Kettle Cooked Sauces
With 300 million pounds of annual kettle capacity, we create both traditional and innovative sauces using fresh ingredients. Our development team formulates everything from classic mother sauces to ethnic-inspired blends, supporting food brands seeking distinctive flavor profiles and consistent product quality for commercial applications.
Artisan Soups
We develop and manufacture premium soups with scalable production capabilities and USDA/FDA licensing. Our culinary team creates both traditional recipes and innovative new formulations, helping restaurant chains differentiate their menus while maintaining operational efficiency through ready-to-use soup solutions.
Breakfast Scrambles
Single-serve breakfast cups combine scrambled eggs, proteins, and roasted vegetables for convenient, heat-and-eat solutions. Available in multiple pre-formulated options or custom-developed recipes, these products help foodservice operators deliver consistent quality while reducing kitchen preparation time.
Craft Beverage Mixers
We create innovative mixers using locally sourced produce and proprietary roasting techniques. Our product development team formulates unique combinations like roasted pineapple-jalapeo margarita mix and tomato-chile bloody mary blends to help beverage programs increase profitability through distinctive, high-quality offerings.
Questions
What types of food products does Haliburton specialize in?
We specialize in fire-roasted vegetables, pickled items, kettle-cooked sauces, artisan soups, breakfast scrambles, dessert sauces, craft beverage mixers, and IQF grain blends.
Do you create custom formulations for specific restaurant needs?
Yes, our culinary and R&D teams develop tailored products to match specific flavor profiles, textures, and operational requirements for both new concepts and existing menu items.
What quality assurance measures do you implement?
We conduct 50 annual independent food safety inspections and maintain on-site microbiology and physical chemistry labs to ensure product consistency and safety.
Are your products available for retail and foodservice?
Our products are designed for both multi-unit restaurant operators and retail brands seeking high-quality, ready-to-use food solutions.
How do you ensure product freshness and shelf life?
Our flash freezing technology preserves freshness while maintaining texture and flavor integrity for extended shelf life in frozen storage conditions.
Can you match existing sauce or soup recipes?
Yes, our development team can analyze and replicate existing formulations while optimizing them for commercial production and consistency.
Videos